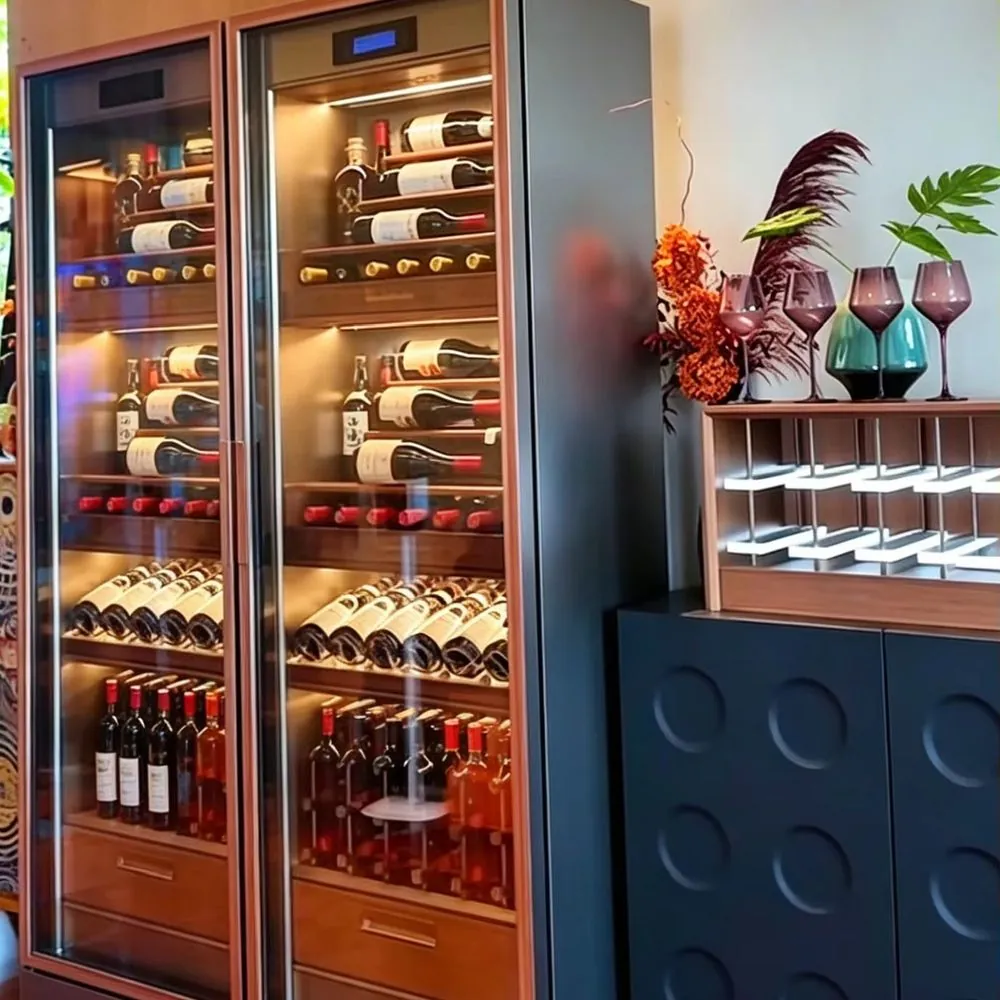
1. Why traditional electroplating and powder coats fail in cellar microclimates
In luxury architectural fit-outs, interior designers frequently specify warm metallic tones—such as champagne gold, brushed brass, warm bronze, or obsidian black—to impart warmth to private wine vaults and hospitality tasting rooms. However, when standard decorative finishing techniques developed for dry residential living rooms are applied inside a temperature-controlled wine preservation enclosure, catastrophic finish failure often occurs within 18 to 36 months.
A dedicated walk-in cellar or luxury wine showcase is not a static ambient room. It operates continuously at 12–14 °C (53–57 °F) and 55–70% relative humidity, generating persistent vapor pressure differentials and microscopic dew-point boundary layers across metal racking, glass door stiles, and structural posts. Under these severe environmental conditions, traditional surface finishing methods exhibit fundamental chemical and mechanical vulnerabilities:
- Electroplated Brass & Gold: Wet chemical electroplating deposits a porous metallic film (typically copper, nickel, and flash gold) over zinc alloys or mild steel. Because the plating is chemically porous, it requires a clear organic lacquer topcoat to prevent oxidation. In high-humidity environments, water vapor penetrates the lacquer through micro-fissures, reacting with the copper sub-layer to produce unsightly green verdigris (copper carbonate), blistering, and total film delamination.
- Powder Coating & Wet Enamels: Organic polymer coatings provide good initial coverage, but their cross-linked polymer chains remain permeable to vapor over multi-year cycles. When heavy wine bottles (1.2–1.4 kg each) are repeatedly loaded and rotated across powder-coated metal cradle rods, abrasive friction shears through the coating, exposing the underlying steel to localized condensation and aggressive crevice corrosion.
- Anodized Aluminum: While anodizing forms an integral aluminum oxide layer, aluminum lacks the structural modulus and weld rigidity required for tall floor-to-ceiling wine posts. Furthermore, dyed anodized surfaces are vulnerable to acid attack from accidental wine spills containing tartaric and malic acids.
For high-end residential estates, Michelin-starred dining venues, and boutique hotel cellars, surface degradation is unacceptable. Specifying our bespoke custom wine cellars requires a finish that matches the 50-year structural lifespan of austenitic stainless steel.
2. The physics of cathodic arc PVD titanium sputtering on SUS304
Physical Vapor Deposition (PVD) is an advanced thin-film coating technology conducted within high-vacuum chambers (typically operating at pressures below 10-3 to 10-5 Torr). Unlike wet chemical baths or electro-static paint sprays, PVD is a purely physical, atomic-level deposition process.
At our manufacturing atelier, PVD processing begins only after all architectural metalwork has been fully laser-cut, CNC-machined, V-grooved, welded, and mechanically grain-polished to either a #4 directional satin hairline or an optical #8 mirror finish:
- Ultrasonic Degreasing & Deionization: Fabricated components undergo multi-stage ultrasonic chemical cleaning, deionized water rinsing, and hot air drying to eliminate all hydrocarbons, polishing compounds, and surface contaminants.
- Vacuum Ion Bombardment (Glow Discharge): Inside the vacuum chamber, inert argon gas is ionized to create a high-density plasma. Energetic argon ions bombard the SUS304 stainless steel substrate, sputter-cleaning the surface at the atomic level and activating its metallic lattice.
- Cathodic Arc Evaporation & Sputtering: High-current electric arcs strike solid high-purity titanium (Ti), zirconium (Zr), or chromium (Cr) target cathodes, vaporizing the metal atoms into a highly ionized metallic vapor stream.
- Reactive Gas Ionization & Deposition: Precisely metered reactive gases (such as ultra-pure Nitrogen N2 or Acetylene C2H2) are introduced into the plasma. The titanium ions combine with the gas ions in flight and condense upon the stainless steel substrate, forming a super-dense, ceramic-hard titanium nitride (TiN) or titanium carbonitride (TiCN) compound film.
Because the deposited titanium atoms penetrate directly into the atomic grain boundaries of the stainless steel, PVD creates an inter-metallic fusion bond with adhesion strengths exceeding 50 to 80 MPa—far surpassing the mechanical adhesion of organic paints or electroplated layers.
3. Layer thickness, surface hardness (HV 2000+), and chromatic consistency
A common misconception is that a thicker coating provides superior protection. In PVD technology, optimal performance is achieved through precise nanometer-scale control:
| Performance Metric | Standard Decorative Electroplating | Architectural PVD on SUS304 | Engineering Benefit |
|---|---|---|---|
| Coating Thickness | 10 – 35 microns (heavy build-up) | 0.5 – 1.2 microns (300–1200 nm) | Preserves microscopic hairline grain & sharp CNC radii without blurring |
| Surface Hardness | 150 – 400 HV (Vickers) | 2,000 – 2,600 HV (Titanium Nitride) | Harder than tool steel; resists bottle scratching and sliding friction |
| Abrasion Resistance | Moderate (scratches easily to base) | Exceptional (ASTM D4060 Taber Index) | Immune to cradle wear across thousands of bottle loading cycles |
| Corrosion Resistance | Fails ASTM B117 < 96 hrs (wet lacquer) | Passes ASTM B117 > 1,000 hrs | Zero pitting or blistering in 70% RH condensing wine room conditions |
| UV Degradation | Lacquer turns yellow/hazy under UV | 100% Inorganic & UV Stable | Zero fading or hue shift under display LED and natural ambient lighting |
By regulating reactive gas ratios during vapor deposition, our engineers produce stable luxury colorways tailored for sophisticated wine storage and commercial bar design:
- Champagne Titanium Gold: Formed through titanium nitride sputtering with balanced nitrogen partial pressure, producing a subtle, pale champagne hue preferred by high-end modern residential architects. Widely deployed across our custom wine cabinets.
- Classic Warm Brass / Yellow Gold: Deep gold TiN stoichiometry designed to evoke classical European brassware without the tarnishing liabilities of raw brass alloy.
- Obsidian Titanium Black: Formed via titanium carbonitride (TiCN) or titanium aluminum nitride (TiAlN), delivering a rich, non-reflective obsidian finish that contrasts dramatically against integrated 2700K warm LED lighting.
- Vintage Bronze & Rose Gold: Zirconium-based and carbon-doped titanium films creating warm coppery reflections for bespoke hospitality tasting salons and commercial bar counters.
4. Zero-VOC off-gassing and food-contact safety for wine preservation
Fine vintage wines sealed with natural cork closures are highly vulnerable to volatile airborne contaminants. Cork bark is gas-permeable by design, facilitating microscopic oxygen transfer over decades of cellaring. If materials within the wine cellar off-gas volatile organic compounds (VOCs), formaldehyde, or aromatic solvents, these molecules will slowly migrate through the cork matrix and taint the wine—causing irreversible chemical spoilage often mistaken for cork taint (TCA).
Traditional solvent-borne wet paints, clear-coat lacquers, and curing resins release residual aromatic hydrocarbons (benzene, toluene, xylene) for months or even years in enclosed, unventilated cold rooms.
5. Engineering sequence: why laser cutting, bending, and welding must precede PVD
One of the most critical design rules that interior specifiers and millwork contractors must understand is the strict irreversibility of the PVD fabrication sequence. Because PVD produces an ultra-hard ceramic compound (HV > 2000), coated metal cannot be subsequently modified using conventional workshop metalworking techniques.
Attempting to post-process PVD-coated raw sheet metal introduces fatal quality flaws:
- Welding Destruction: TIG or laser welding reaches temperatures exceeding 1,450 °C, vaporizing the 1-micron titanium layer and creating prominent discolored heat-tint zones along joint lines that cannot be seamlessly touched up on-site.
- Laser Cut Edge Exposure: Laser-cutting pre-coated sheets exposes a raw, un-coated 1.5–3.0 mm steel core along every cut edge. Under 65% RH humidity, galvanic boundary corrosion can develop between the coated face and the bare edge.
- Micro-Crazing on Tight Bends: While PVD coatings possess slight ductility, executing acute 90-degree CNC press brake bends on pre-coated heavy-gauge sheets can induce micro-fracturing along the outer tensile radius, compromising optical refraction and corrosion protection.
Therefore, our atelier follows a rigorous bespoke production protocol: every racking bracket, glass door frame, bottle support cradle rod, and ceiling suspension post is 100% fabricated, fully welded, hand-ground, and test-assembled in our Foshan atelier. Only after verifying flawless dimensional tolerances is the complete disassembled assembly rack-mounted for ultrasonic cleaning and vacuum PVD deposition.
6. Architectural specification checklist and quality assurance standards
To ensure your architectural tender documents and millwork joinery packages prevent vendor material substitution, incorporate the following enforceable technical clauses into your master specification schedule:
| Specification Parameter | Recommended Master Specification Clause | Inspection & Verification Method |
|---|---|---|
| Base Metal Substrate | Austenitic Stainless Steel Grade SUS304 (UNS S30400 / EN 1.4301). Minimum Ni >= 8.0%, Cr >= 18.0%. Carbon <= 0.08%. Zero 201-grade substitutions permitted. | Mill Test Certificate (EN 10204 Type 3.1) with matching heat numbers & XRF PMI spectral test. |
| Pre-Coating Surface Finish | Mechanically polished #4 directional hairline satin (Ra <= 0.4 um) or #8 optical mirror finish. Degreased and passivated prior to vacuum entry. | Surface roughness profilometer verification & visual inspection under 1000 lux lighting. |
| Coating Technology | Cathodic Arc Physical Vapor Deposition (PVD) Titanium Nitride (TiN) / Titanium Carbonitride (TiCN). Wet electroplating or spray lacquers strictly prohibited. | Vendor chamber batch log documentation & cross-sectional scanning electron microscope (SEM) record. |
| Coating Layer Thickness | Nominal thickness 0.6 – 1.0 micron (+/- 0.15 um) uniform deposition across all visible exterior and interior surfaces. | Calotest spherical crater measurement or X-ray fluorescence (XRF) coating thickness gauge. |
| Adhesion Strength | Class 5B rating per ASTM D3359 cross-hatch tape test; zero flaking or delamination along lattice cuts. | ASTM D3359 test coupon from identical vacuum batch. |
| Corrosion Resistance | Neutral Salt Spray (NSS) ASTM B117 minimum 1,000 hours with zero blistering, pitting, or base metal oxidation. | Certified third-party laboratory salt spray test certificate. |
| Color Consistency | Specified architectural tone (e.g., Champagne Gold) controlled to Delta E (CIE L*a*b*) <= 0.80 across all fabricated components. | Spectrophotometer colorimetric measurement against approved physical master sample. |
For projects integrating complex temperature-controlled enclosures, consult our companion engineering guide on Wine Cellar Temperature and Humidity Specification to coordinate envelope vapor barriers, cooling capacities, and thermal breaks with your interior metal finishes.
7. Frequently asked engineering questions
How do I clean and maintain PVD titanium coated stainless steel surfaces?
Will fingerprints show on brushed champagne gold PVD surfaces?
Can PVD coating be applied to wood or glass components?
Request a Physical PVD Finish Sample Box & CAD Review
Planning a luxury private cellar, restaurant wine wall, or bespoke bar project? Our Foshan engineering desk provides physical PVD metal sample chips (Champagne Gold, Titanium Black, Rose Bronze) and 48-hour CAD shop drawing evaluations.